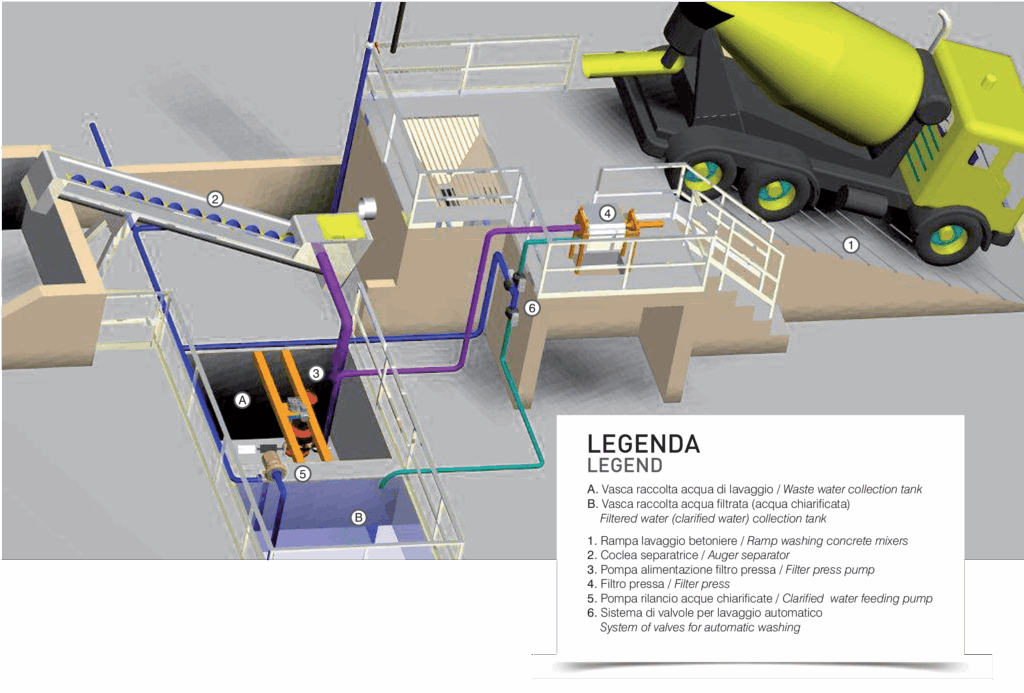
The RAB system is designed for the treatment and recovery of concrete mixer wash water, which typically contains cement residues, sand, aggregates and suspended solids.
The process includes an initial separation stage for the coarser particles using a screw separator, followed by sludge dewatering through a filter press, which produces a solid cake that is easy to handle. The filtered water is recovered and returned to the production cycle, reducing water consumption and operating costs.
The RAB system optimizes material recovery, reduces waste generation and ensures effective management of process wastewater in compliance with environmental regulations.